
In TFT-LCD liquid crystal display modules, there are many defects related to optical display performance, such as:
- whitish light leakage in L0 all-black screens
- COG mura in L0 all-black screens
- border mura in grayscale images
- yellowing, bluing, or blackening of white screens.
There are many causes of these defects, and their impact on LCD display modules and their acceptability vary. After all, some defects are stable and will not worsen over time, while others will become more severe over time.
Therefore, for defects related to optical display performance, it is generally necessary to first identify the true root cause and then conduct a risk assessment based on that cause, so as to avoid incalculable losses.
Today, We would like to share another defect related to the optical display performance of TFT-LCD liquid crystal display modules: LCD yellow mura.
Most readers have encountered LCD yellow mura in their work, but may not be entirely clear about its formation mechanism.
Therefore, in today’s article, we will mainly elaborate on three parts:
- the phenomenon and characteristics of LCD yellow mura
- the formation mechanism of LCD yellow mura
- the common causes and improvement measures for LCD yellow mura
After reading this article,readers can gain a systematic understanding of LCD yellow mura.
Phenomenon and Characteristics of LCD Yellow Mura
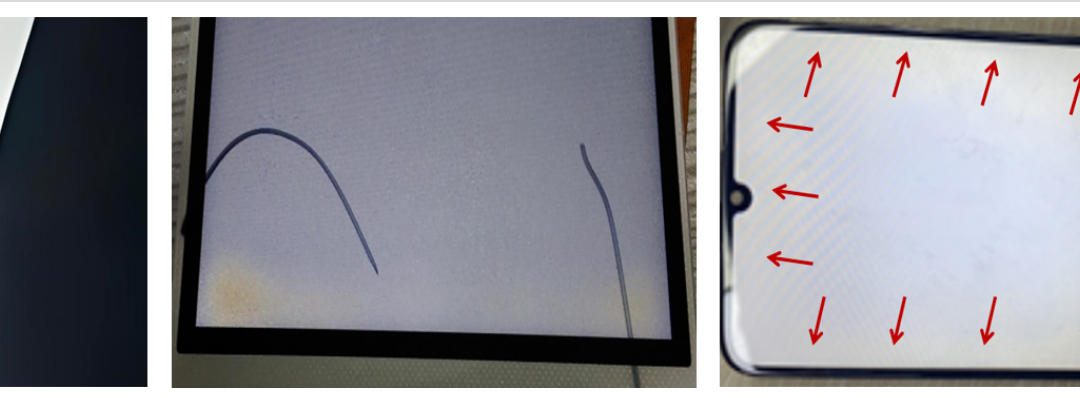
LCD yellow mura generally refers to a phenomenon in which, on a white screen, certain local areas appear yellow or yellowish-brown compared with other areas. LCD yellow mura usually has several key characteristics:
Irregular Shape and Localized Distribution
The shape of LCD yellow mura is irregular, and it is a regional defect. The shapes of LCD yellow mura are usually dot-like, stripe-like, or frame-like. At the same time, LCD yellow mura occurs in localized areas, rather than as yellowing across the entire screen.
Based on the shape and location of the yellow mura, it can usually be classified as dot-like yellowing, localized yellowing at corners, yellowing along the four edges, etc. Different shapes and locations of LCD yellow mura have different causes.

Common manifestations of LCD yellow mura
Irreversibility of LCD yellow mura.
LCD yellow mura is usually caused by physical damage inside the LCD panel after the LCD module is subjected to external compression. Once such damage occurs, it is usually permanent and basically will not disappear on its own. Therefore, LCD yellow mura is irreversible.
Yellow Color Is Usually Obvious and Easily Identifiable
The color of LCD yellow mura is relatively yellowish and obvious. The color of LCD yellow mura usually appears clearly yellow, light yellow, or yellowish-brown, forming a sharp contrast with the surrounding white of the LCD module.
Formation Mechanism of LCD Yellow Mura
Regardless of the phenomenon, location, or severity of LCD yellow mura, its formation mechanism is basically the same. Before discussing the formation mechanism of LCD yellow mura, it is necessary to explain the relationship between LCD panel transmittance and its cell gap.
Relationship Between LCD Transmittance and Cell Gap
LCD transmittance has a certain relationship with cell gap. According to the relationship between LCD transmittance and cell gap, LCD transmittance T is positively correlated with the optical path difference Δnd; that is, when the effective birefringence Δn of the liquid crystal is the same, the larger the LCD cell gap d, the higher the LCD transmittance.
When the LCD cell gap is at its optimal value, the transmittance of the three RGB colors—red, green, and blue. It is also at its optimal value. At this time, the mixed light of the three RGB colors is white, and the LCD module displays a white image.
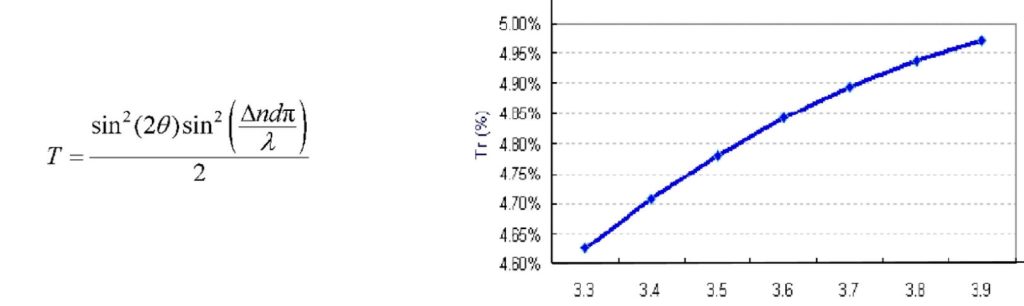
Relationship and variation curve between LCD transmittance and cell gap
Why Increased Cell Gap Causes Yellow Display
Due to the characteristics of the liquid crystal, different LCD cell gaps produce different transmittances for the three RGB colors.
When the LCD cell gap increases, the transmittance of blue light B decreases significantly, while red light R and green light G still maintain a certain transmittance. The mixture of red light R and green light G is yellow light, so the LCD appears yellow.
When the LCD cell gap decreases, the transmittance of blue light B is the highest, so the LCD appears blue.
Therefore, the formation mechanism of LCD yellow mura is: it is caused by an increase in the LCD cell gap. The increase in LCD cell gap is basically caused by external compression on the LCD module, which causes the liquid crystal inside the cell to accumulate in the peripheral areas around the compressed region. The cell gap at the locations where the liquid crystal accumulates is forced larger, ultimately causing yellowing in the LCD module.

Illustration of the formation mechanism of LCD yellow mura
Common Causes and Improvement Measures for LCD Yellow Mura
As explained earlier, the formation mechanism of LCD yellow mura is basically that the LCD module is subjected to external compression. It causes the LCD cell gap to increase, leading to yellowing in the LCD module.
Throughout the entire manufacturing process and final product testing of LCD modules, compression forces on the LCD module come from many sources. However, the common compression forces that cause LCD yellow mura mainly come from:
- compression during final product mechanical testing
- compression during OCA lamination
- compression during LCD cell assembly etc.
Compression on the LCD during complete-device mechanical testing (peripheral yellowing):
After assembly of the complete device, various mechanical tests are usually performed to evaluate its mechanical performance. These tests generally include tumble, micro-drop, directional drop, compression, and so on.
During complete-device mechanical testing, many factors can cause the LCD module to develop yellow mura after being compressed by the device housing, such as:
- The amount of liquid crystal inside the LCD panel
- Main PS height
- PS density
- The flatness of the LCD module and the device housing
- The matching clearance in the Z-direction
- The strength of the device housing
a. Causes of peripheral yellowing:
The specific process by which yellow mura occurs in the LCD module after complete-device mechanical testing is as follows :
If the overall thickness of the LCD module is on the thick side or its flatness is poor, the clearance between it and the device housing in the Z-direction will be too small. Repeated complete-device mechanical tests will cause the housing to compress the LCD module.

Illustration of the fit between the device housing and the LCD module
When the LCD module is compressed, the Main PS in the central area of the LCD panel is usually compressed, causing the cell gap in the central area to decrease. However, the PS spacers in the sealant around the LCD periphery provide support, so the Main PS around the periphery is basically not compressed.
After the central area of the LCD is compressed and its cell gap decreases, the liquid crystal flows toward the periphery and accumulates there, forcing the cell gap at the LCD edges to increase. This ultimately causes peripheral yellowing in the LCD.

Comparison of the LCD module before and after compression
b. Improvement measures for peripheral yellowing:
Improvement measures for peripheral yellowing in the LCD are generally divided into two aspects:
- one is to improve the LCD panel itself, that is, to improve the stability of the LCD cell gap;
- the other is to improve the matching between the LCD module and the housing.
Common improvement measures are as follows:
Reduce the amount of liquid crystal in the LCD cell. When the amount of liquid crystal is reduced (the ability of the liquid crystal to support the cell gap weakens, and support mainly relies on PS), the Main PS will first be compressed in its initial state, thereby reducing the step difference between it and the Sub PS.
When the LCD is subjected to external compression, the Main PS can be quickly compressed and deformed. At this point, the Sub PS can quickly provide effective support to resist the external force.
Keep the amount of liquid crystal unchanged and increase the height of the Main PS. With a taller Main PS, when the LCD is subjected to external compression, the compression amount of the Main PS effectively increases.
This can suppress the decrease in cell gap in the central area of the LCD during complete-device mechanical testing, ultimately ensuring the stability of the cell gap in all areas within the LCD cell.
Increase the PS density per unit area. A higher PS density can improve the LCD’s resistance to compression and deformation, ensuring the stability of the cell gap in all areas within the LCD cell.
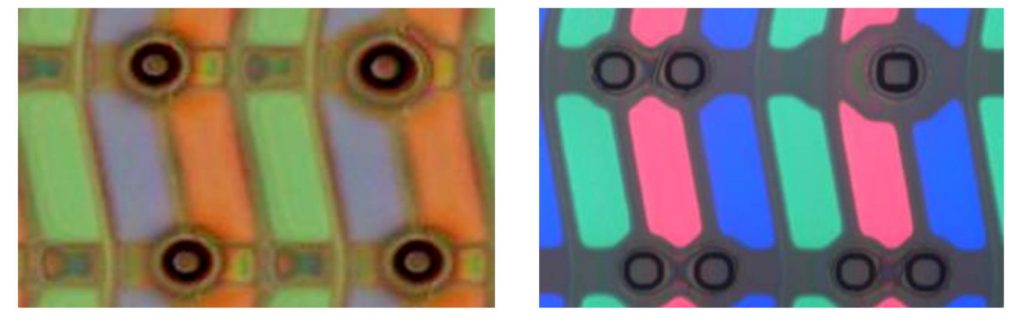
Comparison of low and high PS density in the LCD cell
Ensure the Z-direction clearance between the LCD module and the device housing. Controlling the overall thickness of the LCD module toward the lower-middle end of the tolerance range, managing the flatness of both the LCD module and the device housing, and increasing the strength of the device housing are also common improvement measures for reducing peripheral yellowing of the LCD.
Compression on the LCD during OCA full lamination (localized yellowing):
Uneven local areas and residual stress during OCA lamination are also common causes of localized LCD yellowing.
In addition, interference inside the LCD module, there are also common causes of localized LCD yellowing, such as:
- excessive silicone adhesive thickness
- UV adhesive and conductive silver paste being higher than the upper polarizer and interference between the LCD module and the device housing
Due to space limitations, these will not be discussed in detail here.
a. Causes of localized yellowing:
Taking uneven local areas after OCA lamination as an example, when the force applied during OCA soft-to-hard lamination is uneven, localized recesses form in the OCA. During hard-to-hard lamination and vacuum evacuation, these recessed areas pull on the LCD, increasing the cell gap, it is similar to a suction-cup effect.
At this point, the transmittance of blue light B drops markedly, while red light R and green light G still maintain a certain transmittance, ultimately causing localized yellow mura in the LCD.
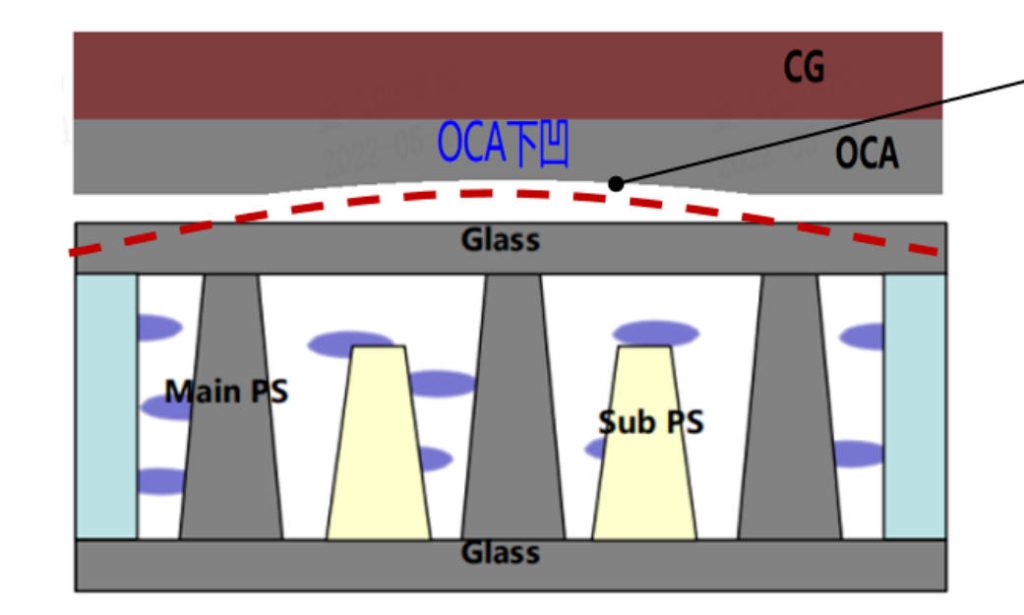
Illustration of the mechanism by which uneven OCA causes LCD yellowing
b. Improvement measures for localized yellowing:
Conduct DOE validation during the OCA full-lamination process to prevent localized yellowing caused by uneven OCA areas and residual stress.
During soft-to-hard lamination, validate and establish the optimal lamination pressure and speed, and ensure the flatness of the lamination platform.
During hard-to-hard lamination, validate and establish the optimal lamination pressure, lamination time, and vacuum level, and confirm the parallelism of the lamination chamber, thereby reducing the risk of localized yellowing caused by OCA compression on the LCD.
Compression on the LCD during cell assembly (dot-like yellowing):

Dot-like yellowing caused by compression from foreign particles during LCD cell assembly is relatively rare. It is sufficient to focus on controlling cleanliness during the cell assembly process.
The formation mechanism of dot-like LCD yellowing is similar to the above: during the pairing and assembly of the CF and TFT substrates into a cell, equipment wear generates foreign particles. These foreign particles lift the LCD cell, and at the locations lifted by the foreign particles, the cell gap increases, ultimately causing dot-like yellowing.
Summary:
LCD yellow spot defects are mainly caused by local Cell Gap enlargement.
Although the appearance may vary, including:
- Edge yellowing
- Local yellow patches
- Dot-shaped yellow spots
the fundamental optical mechanism is similar:
Mechanical stress → Cell Gap variation → RGB transmittance imbalance → Yellow appearance
The main causes and improvement directions can be summarized as follows:
| Root Cause | Typical Appearance | Main Improvement Methods |
| Mechanical compression during product reliability testing | Four-side yellowing | Optimize LCD structure, increase PS support, control module thickness and housing clearance |
| OCA bonding stress or uneven lamination | Local yellow spots | Optimize bonding pressure, speed, vacuum level, platform flatness and chamber parallelism |
| Foreign particles during Cell assembly | Dot-shaped yellow spots | Improve cleanroom control and reduce particle contamination |
For TFT-LCD module manufacturers and system product engineers, preventing yellow spots requires cooperation between:
- LCD Cell design
- Module mechanical design
- OCA bonding process
- Final product structural design
- Reliability testing conditions
A stable Cell Gap distribution is the key factor for maintaining consistent optical performance.